


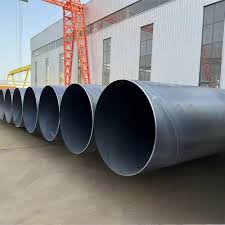
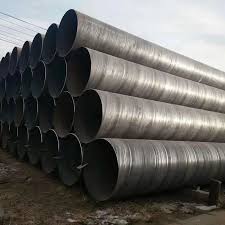
GB/T 3091 Q235B is the most common and widely used material specification for manufacturing Spiral Submerged Arc Welded (SSAW) steel pipes [citation:1, citation:2, citation:3, citation:6, citation:8, citation:10]. This combination represents the standard workhorse product for low-pressure fluid transmission and general structural applications under the Chinese national standard, offering an excellent balance of strength, weldability, and cost [citation:5, citation:7, citation:8].
The designation "GB/T 3091 Q235B Spiral Submerged Arc Pipe" combines the most popular carbon structural steel grade (Q235B) with the spiral welding process for large-diameter, cost-effective applications where reliable performance is required [citation:8, citation:10].
📋 Key Specifications for GB/T 3091 Q235B SSAW Pipe
The table below summarizes the primary specifications for this product, based on comprehensive industry data [citation:1, citation:2, citation:3, citation:4, citation:5, citation:6, citation:8, citation:10].
| Attribute | Description |
|---|---|
| Standard | GB/T 3091: "Welded steel pipes for low pressure liquid delivery" (current version: GB/T 3091-2015; new version GB/T 3091-2025 effective October 2025) [citation:2, citation:4, citation:8, citation:9]. |
| Scope | Applicable to water, air, heating steam, gas, and other low-pressure fluid transmission [citation:2, citation:3, citation:4, citation:6, citation:8]. |
| Steel Grade | Q235B: The most common carbon structural steel grade. The "Q" stands for "屈服强度" (yield strength), "235" indicates the minimum yield strength in MPa, and "B" denotes the quality grade with specified impact requirements at room temperature (+20°C) [citation:1, citation:2, citation:5, citation:7]. |
| Base Material Standard | GB/T 700: Carbon Structural Steels [citation:1, citation:2, citation:4, citation:5]. |
| Manufacturing Process | Spiral Submerged Arc Welding (SSAW/HSAW) : Formed from hot-rolled steel coil at room temperature using five-roll forming, with the weld seam running continuously in a spiral. Welded using double-sided automatic submerged arc welding (inside and outside) [citation:2, citation:4, citation:8, citation:10]. |
| Chemical Composition (max %) [citation:1, citation:4, citation:5] | Carbon (C): ≤ 0.20% Manganese (Mn): 0.30-0.70% Silicon (Si): ≤ 0.30-0.35% Phosphorus (P): ≤ 0.045% Sulfur (S): ≤ 0.045% |
| Mechanical Properties (min) [citation:1, citation:2, citation:5, citation:7, citation:9] | Yield Strength (t ≤ 16mm): 235 MPa Yield Strength (t > 16mm): 225 MPa Tensile Strength: 370-500 MPa Elongation (D > 168.3mm): ≥ 20% Charpy Impact: 27 J minimum at +20°C [citation:2, citation:5, citation:7] |
| Typical Size Range [citation:3, citation:6, citation:8, citation:10] | Outside Diameter: 219 mm to 4064 mm (approx. 8" to 160") for SSAW; smaller diameters available as ERW Wall Thickness: 2.0 mm to 26 mm for SSAW [citation:6, citation:10] Length: 3 m to 12 m standard; up to 25 m available [citation:3, citation:6, citation:10] |
| Key Testing Requirements [citation:2, citation:4, citation:8, citation:10] | Chemical analysis; tensile test; flattening test; bend test; hydrostatic test (each pipe); non-destructive testing (ultrasonic or X-ray of weld seam - standard practice). Charpy impact testing is required for Grade B at +20°C [citation:2, citation:5]. |
| Common Applications [citation:3, citation:5, citation:6, citation:7, citation:8, citation:10] | Water transmission; municipal water supply and drainage; natural gas distribution (low pressure); heating steam lines; compressed air systems; agricultural irrigation; fire protection systems; structural applications; piling foundations; general construction. |
| Certification | Mill Test Certificate typically to EN 10204 Type 3.1 or equivalent, with full test results and traceability records [citation:2, citation:6, citation:8]. |
📊 GB/T 3091 Grade Comparison
Q235B is the most common strength grade in the GB/T 3091 specification. The table below shows its position relative to other grades [citation:1, citation:2, citation:5, citation:7, citation:9]:
| Grade | Yield Strength (MPa) min (t ≤ 16mm) | Tensile Strength (MPa) min | Elongation % (D > 168.3mm) | Relative Strength vs. Q235B | Key Feature | Typical Application |
|---|---|---|---|---|---|---|
| Q195 | 195 | 315 | 20 | -17% | Most economical | Non-critical, cost-driven applications |
| Q215B | 215 | 335 | 20 | -9% | Good ductility | Light structures, cold bending applications |
| Q235B | 235 | 370 | 20 | Baseline | Balanced properties | General construction - MOST COMMON |
| Q275B | 275 | 410 | 18 | +17% | Higher strength | Moderate load-bearing structures |
| Q345B | 345 | 470 | 18 | +47% | High strength | Heavy-duty structural applications |
📏 Dimensional Specifications
GB/T 3091 specifies the following typical tolerances for SSAW pipes [citation:1, citation:2, citation:3, citation:4, citation:6, citation:8]:
| Parameter | Tolerance |
|---|---|
| Outside Diameter (OD ≤ 508mm) | ±0.75% of specified diameter |
| Outside Diameter (OD > 508mm) | ±1.0% of specified diameter |
| Wall Thickness (t ≤ 5.0mm) | ±0.5mm [citation:3, citation:6] |
| Wall Thickness (5.0mm < t < 15.0mm) | ±0.1t [citation:3, citation:6] |
| Wall Thickness (t ≥ 15.0mm) | ±1.5mm [citation:3, citation:6] |
| Straightness (OD > 168.3mm) | ≤ 0.2% of total length |
| Length (fixed lengths) | +100mm / -0mm |
| End Finish | Plain ends standard; beveled ends for wall thickness > 4mm (30° angle, 1.6mm root face) |
Standard Diameter Range for SSAW: 219mm to 4064mm (8" to 160") [citation:3, citation:6, citation:8, citation:10]
🔍 Key Points to Understand
What "GB/T 3091 Q235B" Means: This is the Chinese national standard for low-pressure fluid transmission pipes using the most popular carbon steel grade. The "B" suffix is significant-it guarantees Charpy V-notch impact energy of 27 Joules at room temperature (+20°C) , making it suitable for general structural applications where some toughness is required [citation:2, citation:5, citation:7].
Why Q235B is the Most Common Grade: Q235B offers the best balance of strength, weldability, and cost for a wide range of applications [citation:7, citation:8]. It is the default choice for most general-purpose piping and structural applications in China, equivalent to ASTM A36 in US standards and S235JR in European standards .
Q235B vs. Q235A: The key difference is impact testing:
Q235A: No mandatory Charpy impact testing
Q235B: Mandatory Charpy impact testing at +20°C, 27J minimum [citation:2, citation:5]
Choose Q235B for any application requiring toughness assurance.
SSAW Advantages for Q235B: The spiral welding process offers specific benefits for large-diameter pipes [citation:8, citation:10]:
Large Diameter Capability: Can economically produce pipes up to 160" diameter
Cost Efficiency: Lower cost than longitudinal welding for large diameters
Long Lengths: Up to 25m lengths reduce field joints
Material Efficiency: Can use narrower steel strips to produce large-diameter pipes
🔧 Manufacturing Process for GB/T 3091 Q235B SSAW Pipe
The manufacturing process follows well-established SSAW production methods [citation:4, citation:8, citation:10]:
| Step | Description |
|---|---|
| 1. Raw Material Preparation | Hot-rolled steel coils meeting Q235B chemistry requirements are leveled, inspected, and edge-milled [citation:4, citation:8]. |
| 2. Spiral Forming | The steel strip is continuously formed into a cylindrical shape at a specific helix angle at room temperature using five-roll forming technology [citation:4, citation:8, citation:10]. |
| 3. Submerged Arc Welding | Double-sided automatic submerged arc welding (inside and outside) creates the spiral seam with full penetration. Internal and external welds overlap completely [citation:4, citation:8, citation:10]. |
| 4. Non-Destructive Testing | 100% ultrasonic or X-ray inspection of the weld seam is standard practice [citation:8, citation:10]. |
| 5. Hydrostatic Testing | Each pipe individually tested to verify pressure integrity (typically ≥1.0 MPa per project requirements) [citation:5, citation:8]. |
| 6. Mechanical Testing | Tensile tests, flattening tests, bend tests, and mandatory Charpy impact testing for Grade B [citation:2, citation:4]. |
| 7. End Finishing | Ends prepared (plain or beveled) for field welding; beveled ends for wall thickness > 4mm [citation:1, citation:4]. |
| 8. Coating | Optional external coatings (varnish, bitumen, FBE, 3LPE) and galvanizing available (OD ≤ 508mm) [citation:2, citation:4]. |
🏭 Applications
GB/T 3091 Q235B SSAW pipes are the standard choice for a vast range of applications [citation:3, citation:5, citation:6, citation:7, citation:8, citation:10]:
| Application | Description | Why Q235B is Chosen |
|---|---|---|
| Water Transmission | Municipal water supply, drainage systems, irrigation | Reliable performance, economical |
| Natural Gas Distribution | Low-pressure gas pipelines | Guaranteed toughness at room temperature |
| Heating Systems | District heating, steam lines (low pressure) | Good weldability for field joints |
| Fire Protection Systems | Fire water mains, sprinkler systems | Adequate strength, proven reliability |
| Structural Applications | Piling, bridge supports, building frames | Excellent balance of strength and cost |
| Agricultural Irrigation | Large-scale irrigation systems | Cost-effective for large diameters |
| Industrial Piping | Compressed air, process water, cooling systems | Versatile and widely available |
📝 Important Considerations
Standard Version: The current version is GB/T 3091-2015. A new version GB/T 3091-2025 will be effective from October 1, 2025, with updated requirements including higher elongation (≥23% for Q235B) and potential low-temperature impact testing options [citation:4, citation:8, citation:9]. When ordering, specify the required version year.
Pressure Rating: Typical design pressure for Q235B SSAW pipes is ≤1.6 MPa . A water utility tender specified minimum pressure rating of 1.0 MPa for Q235B spiral pipes .
Coating Options: Pipes can be supplied with various coatings [citation:2, citation:4, citation:5]:
Galvanized: For corrosion protection (OD ≤ 508mm only) [citation:2, citation:4]
FBE/3LPE: For buried pipelines
Bitumen coating: For buried service
Internal lining: Cement mortar, epoxy for water service
International Approximations: Q235B is roughly equivalent to:
ASTM A36 (250 MPa yield - slightly higher)
EN 10025 S235JR (235 MPa yield)
ISO 630 E235B
Complete Specification: When ordering, specify [citation:3, citation:5, citation:8]:
GB/T 3091, Grade Q235B, SSAW (spiral welded), Size (OD x WT), Length, End Finish
Standard version: [e.g., GB/T 3091-2015]
Pressure rating: [e.g., 1.0 MPa, 1.6 MPa]
Coating requirements: [e.g., bare, galvanized, 3LPE]
📝 Summary
GB/T 3091 Q235B Spiral Submerged Arc Welded pipes are the standard, most common, and widely available choice for large-diameter, low-pressure fluid transmission and structural applications under the Chinese national standard [citation:1, citation:2, citation:5, citation:6, citation:7, citation:8, citation:10]. With minimum yield strength of 235 MPa, these pipes offer the optimal balance of strength, weldability, and cost for a vast range of applications from water supply and gas distribution to structural supports and piling foundations [citation:5, citation:7, citation:8].
The "B" quality grade guarantees Charpy impact toughness of 27 Joules at room temperature (+20°C), making Q235B suitable for general construction and applications where some impact resistance is needed [citation:2, citation:5]. This is the key difference from Q235A, which has no mandatory impact testing .
Available in diameters from 219mm to over 4000mm with wall thicknesses to 26mm and lengths up to 25m, these pipes are produced using the cost-effective SSAW manufacturing process with double-sided submerged arc welding, ensuring reliable weld quality [citation:4, citation:8, citation:10].
Q235B is the default grade for most general-purpose piping in China, equivalent to ASTM A36 and S235JR internationally. For applications requiring even higher strength, consider upgrading to Q275B or Q345B [citation:1, citation:2, citation:5].
When ordering, ensure you clearly indicate the complete standard with version year (current GB/T 3091-2015, or upcoming GB/T 3091-2025 from October 2025), grade Q235B, manufacturing process (SSAW), required dimensions, and any coating or supplementary requirements based on your specific application [citation:3, citation:5, citation:8].


