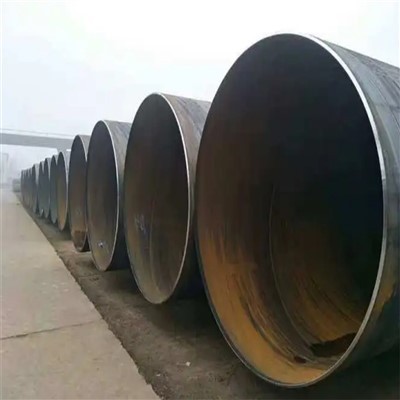
Hey there! As a carbon steel tube supplier, I've seen my fair share of issues when it comes to welding carbon steel tubes. One of the most common and frustrating problems is the development of cracks during the welding process. Cracks can compromise the integrity of the welded joint, leading to potential failures and safety hazards. In this blog post, I'll share some tips on how to avoid cracks in carbon steel tubes during welding.
Understanding the Causes of Cracks
Before we dive into the prevention methods, it's important to understand what causes cracks in carbon steel tubes during welding. There are several factors that can contribute to crack formation, including:
- Hydrogen Embrittlement: Hydrogen can be introduced into the weld metal during the welding process, especially when using certain welding consumables or in the presence of moisture. Hydrogen can cause the steel to become brittle, increasing the risk of cracking.
- Residual Stress: Welding generates heat, which causes the metal to expand and contract. This expansion and contraction can create residual stress in the welded joint, which can lead to cracking over time.
- Poor Welding Technique: Incorrect welding parameters, such as improper welding speed, current, or voltage, can result in a poor-quality weld that is more prone to cracking.
- Inadequate Preheating and Post-Weld Heat Treatment: Carbon steel tubes may require preheating before welding to reduce the risk of cracking. Similarly, post-weld heat treatment can help relieve residual stress and improve the mechanical properties of the welded joint.
- Contamination: The presence of contaminants, such as oil, grease, rust, or dirt, on the surface of the carbon steel tubes can affect the quality of the weld and increase the risk of cracking.
Prevention Methods
Now that we understand the causes of cracks, let's look at some effective prevention methods:
1. Select the Right Welding Consumables
- Choose welding consumables that are compatible with the carbon steel tubes you are welding. The consumables should have a similar chemical composition to the base metal to ensure good weld quality.
- Use low-hydrogen welding consumables to minimize the risk of hydrogen embrittlement. These consumables are designed to reduce the amount of hydrogen introduced into the weld metal.
2. Prepare the Surface Properly
- Clean the surface of the carbon steel tubes thoroughly before welding to remove any contaminants. You can use a wire brush, grinder, or chemical cleaner to clean the surface.
- Remove any rust, scale, or paint from the welding area to ensure good fusion between the base metal and the weld metal.
3. Preheat the Tubes
- Preheating the carbon steel tubes before welding can help reduce the risk of cracking. Preheating slows down the cooling rate of the weld metal, which reduces the formation of residual stress and hydrogen embrittlement.
- The preheating temperature depends on the thickness and composition of the carbon steel tubes. Consult the welding procedure specification (WPS) or a welding engineer to determine the appropriate preheating temperature.
4. Use the Correct Welding Parameters
- Set the welding parameters, such as welding speed, current, and voltage, according to the thickness and composition of the carbon steel tubes. Using incorrect parameters can result in a poor-quality weld that is more prone to cracking.
- Maintain a consistent welding speed and travel angle to ensure uniform heat input and good fusion between the base metal and the weld metal.
5. Employ Proper Welding Techniques
- Use a welding technique that minimizes the amount of heat input and reduces the risk of residual stress. For example, the backstep welding technique can be used to reduce the heat input and distribute the stress more evenly.
- Avoid over-welding or under-welding, as both can lead to cracking. Over-welding can cause excessive heat input and residual stress, while under-welding can result in a weak weld joint.
6. Perform Post-Weld Heat Treatment
- Post-weld heat treatment (PWHT) can help relieve residual stress and improve the mechanical properties of the welded joint. PWHT involves heating the welded joint to a specific temperature and holding it for a certain period of time before cooling it slowly.
- The PWHT temperature and time depend on the thickness and composition of the carbon steel tubes. Consult the WPS or a welding engineer to determine the appropriate PWHT parameters.
7. Control the Cooling Rate
- After welding, control the cooling rate of the welded joint to prevent rapid cooling, which can increase the risk of cracking. You can use insulation or slow cooling methods to control the cooling rate.
- Avoid quenching the welded joint in water or other coolants, as this can cause rapid cooling and increase the risk of cracking.
Examples of Our Products
As a carbon steel tube supplier, we offer a wide range of high-quality products that are suitable for various welding applications. Here are some examples of our products:


- 316 Stainless Steel Welded Pipe: This pipe is made of 316 stainless steel, which offers excellent corrosion resistance and high strength. It is suitable for use in various industries, including chemical, food processing, and marine.
- S235JR Straight Seam Welded Steel Pipe: This pipe is made of S235JR steel, which is a low-carbon steel with good weldability and formability. It is commonly used in structural applications, such as building construction and machinery manufacturing.
- A36 Welded Carbon Steel Pipe: This pipe is made of A36 carbon steel, which is a widely used structural steel with good strength and ductility. It is suitable for use in various applications, including bridges, buildings, and automotive.
Conclusion
Cracks in carbon steel tubes during welding can be a serious problem, but they can be avoided by following the prevention methods outlined in this blog post. By selecting the right welding consumables, preparing the surface properly, preheating the tubes, using the correct welding parameters, employing proper welding techniques, performing post-weld heat treatment, and controlling the cooling rate, you can ensure high-quality welds that are free from cracks.
If you're in the market for high-quality carbon steel tubes for your welding projects, don't hesitate to contact us. We're here to help you find the right products for your needs and provide you with expert advice and support. Let's work together to ensure the success of your welding projects!
References
- Welding Handbook, American Welding Society
- AWS D1.1 Structural Welding Code - Steel, American Welding Society
- ASME Boiler and Pressure Vessel Code, American Society of Mechanical Engineers