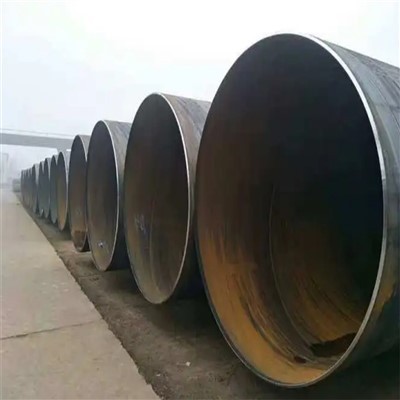
As a supplier of Seam Steel Pipe, I'm excited to share with you the detailed production process of SSAW (Spiral Submerged Arc Welded) Seam Steel Pipe. Understanding this process is crucial for anyone involved in the steel pipe industry, whether you're a buyer, engineer, or simply interested in the manufacturing behind these essential products.
Raw Material Preparation
The first step in the production of SSAW Seam Steel Pipe is the selection and preparation of raw materials. We typically use high - quality steel coils as our base material. These steel coils are sourced from reputable steel mills that adhere to strict quality standards. The chemical composition and mechanical properties of the steel coils are carefully inspected to ensure they meet the requirements for the specific type of SSAW pipe we are producing.
The width and thickness of the steel coils are determined based on the desired diameter and wall thickness of the final pipe. For example, if we are manufacturing a large - diameter pipe, we will choose wider and thicker steel coils. Once the appropriate steel coils are selected, they are uncoiled and leveled to remove any internal stresses and ensure a flat surface for the subsequent forming process.
Pipe Forming
After the raw materials are prepared, the steel strip is fed into the pipe forming machine. In the case of SSAW pipes, the forming process involves spirally winding the steel strip into a cylindrical shape. The forming machine uses a series of rollers to gradually bend the steel strip along a helical path, creating a continuous spiral seam.
The key to a successful forming process is maintaining a consistent spiral angle and ensuring that the edges of the steel strip are properly aligned. This is achieved through precise control of the roller positions and the speed of the forming machine. Any deviation in the spiral angle or misalignment of the edges can lead to defects in the final pipe, such as uneven wall thickness or poor weld quality.
Welding
Once the pipe is formed, the next step is welding. SSAW pipes are typically welded using the submerged arc welding (SAW) process. SAW is a highly efficient and reliable welding method that produces high - quality welds with excellent mechanical properties.
In the SAW process, a granular flux is deposited on the weld joint, and an electric arc is struck between the welding wire and the steel strip. The flux serves several important functions. It protects the weld pool from atmospheric contamination, provides a stable arc, and helps to control the cooling rate of the weld, which is crucial for the formation of a strong and defect - free weld.
The welding parameters, such as the welding current, voltage, and welding speed, are carefully adjusted based on the thickness of the steel strip and the type of flux used. Multiple passes of welding may be required for thicker - walled pipes to ensure full penetration of the weld joint. After welding, the pipe is inspected for any weld defects, such as porosity, cracks, or lack of fusion, using non - destructive testing methods such as ultrasonic testing or X - ray inspection.
Heat Treatment
Heat treatment is an important step in the production of SSAW Seam Steel Pipe, especially for pipes that require high strength and good toughness. Heat treatment can improve the mechanical properties of the pipe by relieving internal stresses, refining the grain structure, and enhancing the hardness and strength of the weld and the base metal.
There are several types of heat treatment processes that can be used, including normalizing, quenching, and tempering. The choice of heat treatment process depends on the specific requirements of the pipe. For example, if the pipe is used in high - pressure applications, quenching and tempering may be required to achieve the desired strength and toughness.
During the heat treatment process, the pipe is heated to a specific temperature and held at that temperature for a certain period of time, followed by controlled cooling. The heating and cooling rates are carefully controlled to ensure uniform heat treatment throughout the pipe. After heat treatment, the pipe is again inspected to ensure that the desired mechanical properties have been achieved.
Pipe Cutting and Finishing
Once the heat treatment is completed, the pipe is cut to the desired length. This is typically done using a cutting machine, such as a saw or a plasma cutter. The cutting process must be precise to ensure that the pipe ends are square and free of burrs.
After cutting, the pipe undergoes a series of finishing operations, including beveling the pipe ends, cleaning the surface, and applying a protective coating. Beveling the pipe ends is necessary for easy installation and welding during the pipeline construction. The surface cleaning process removes any dirt, rust, or scale from the pipe surface, which can improve the adhesion of the protective coating.
The protective coating is applied to prevent corrosion and extend the service life of the pipe. There are various types of protective coatings available, such as epoxy coatings, polyethylene coatings, and zinc coatings. The choice of coating depends on the operating environment and the specific requirements of the pipeline.
Quality Control
Throughout the entire production process, strict quality control measures are implemented to ensure that the SSAW Seam Steel Pipe meets the highest standards of quality. In addition to the non - destructive testing methods mentioned earlier, visual inspection is also carried out at every stage of production to detect any obvious defects, such as surface scratches, dents, or unevenness.
Mechanical testing, such as tensile testing, hardness testing, and impact testing, is also performed on samples taken from the pipe to verify its mechanical properties. The pipe is also tested for its hydrostatic pressure to ensure that it can withstand the specified operating pressure without leakage.
Applications of SSAW Seam Steel Pipe
SSAW Seam Steel Pipe is widely used in various industries, including oil and gas transportation, water supply and drainage, structural engineering, and piling. In the oil and gas industry, SSAW pipes are commonly used for transporting crude oil, natural gas, and refined products over long distances. Our API 5L X65 X70 Welded Pipe is specifically designed to meet the high - performance requirements of oil and gas pipelines.
In the water supply and drainage industry, SSAW pipes are used for building water transmission and distribution systems. The A 106 STEEL PIPE is a popular choice for these applications due to its excellent corrosion resistance and mechanical properties.
In structural engineering, SSAW pipes are used as columns, beams, and braces in buildings and bridges. The High Strength Q235B Welded Pipe With Good Price is often used in these applications because of its high strength - to - weight ratio and good weldability.


Conclusion
The production process of SSAW Seam Steel Pipe is a complex and highly technical process that involves multiple steps, from raw material preparation to final finishing. Each step is crucial for ensuring the quality and performance of the final product. As a Seam Steel Pipe supplier, we are committed to producing high - quality SSAW pipes that meet the diverse needs of our customers.
If you are interested in purchasing SSAW Seam Steel Pipe or have any questions about our products, please feel free to contact us for further discussion and negotiation. We look forward to serving you and providing you with the best solutions for your steel pipe needs.
References
- ASME Boiler and Pressure Vessel Code
- API 5L Specification for Line Pipe
- ASTM Standards for Steel Pipe