Hey there! As a supplier of ERW Steel Pipes, I often get asked about different inspection methods. One that comes up quite a bit is magnetic particle inspection. So, let's dig into what magnetic particle inspection of ERW Steel Pipes is all about.
What Are ERW Steel Pipes?
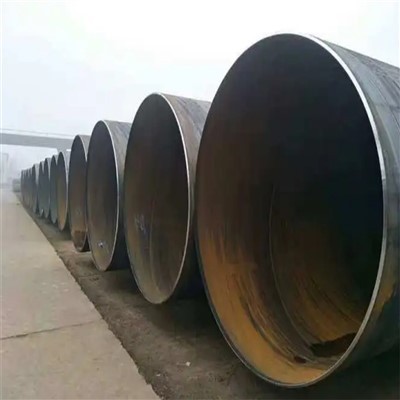
Before we jump into magnetic particle inspection, let me quickly tell you about ERW Steel Pipes. Electric Resistance Welded (ERW) Steel Pipes are made by rolling steel sheets into a tubular shape and then welding the edges together using an electric current. These pipes are super versatile and are used in a wide range of industries, from construction to oil and gas. We offer different types of ERW Steel Pipes, like the S355 Electric Resistance Carbon Steel Pipe, which is great for structural applications, and the API 5CT K55 OCTG Tube, used in the oil and gas sector.
Why Inspection Matters
Inspecting ERW Steel Pipes is crucial. You see, even a tiny defect in a pipe can lead to big problems down the line. In industries where safety and reliability are top priorities, like oil and gas or construction, a faulty pipe can cause leaks, structural failures, and other disasters. That's why we use various inspection methods to make sure our pipes meet the highest quality standards. And one of the most effective methods for detecting surface and near - surface defects in ferromagnetic materials (like most ERW Steel Pipes) is magnetic particle inspection.
How Magnetic Particle Inspection Works
Magnetic particle inspection, often called MPI, is based on the principle of magnetic fields. When a ferromagnetic material (like our ERW Steel Pipes) is magnetized, the magnetic field lines run through the material in an orderly way. But if there's a defect, like a crack or a porosity, the magnetic field gets disrupted. The defect acts as a barrier, causing the magnetic field lines to "leak" out of the material at the site of the defect.
Here's a step - by - step breakdown of how we do MPI on our ERW Steel Pipes:
Step 1: Cleaning the Pipe
First, we need to clean the surface of the pipe thoroughly. Any dirt, grease, or rust can interfere with the inspection. We use solvents or mechanical methods to make sure the pipe surface is clean and ready for the next step.
Step 2: Magnetizing the Pipe
There are different ways to magnetize the pipe. We can use a permanent magnet, an electromagnet, or a combination of both. The goal is to create a strong enough magnetic field in the pipe. The direction of magnetization depends on the expected orientation of the defects. For example, if we suspect longitudinal defects, we'll magnetize the pipe axially.
Step 3: Applying Magnetic Particles
Once the pipe is magnetized, we apply magnetic particles to the surface. These particles can be in the form of a dry powder or a wet suspension. When the magnetic particles come in contact with the "leaked" magnetic field at the site of a defect, they are attracted to it and form a visible indication. The particles cluster together, making the defect easy to see.
Step 4: Inspection
After applying the magnetic particles, we carefully examine the pipe surface. We look for any patterns or clusters of particles that indicate a defect. The size, shape, and location of the particle clusters can give us clues about the nature of the defect. For example, a long, thin cluster might indicate a crack, while a more irregular cluster could be a porosity.
Step 5: Demagnetizing the Pipe
Once the inspection is done, we demagnetize the pipe. Leaving the pipe magnetized can cause problems later, like attracting metal debris or interfering with other equipment. We use a demagnetizing coil or a similar device to gradually reduce the magnetic field in the pipe to near - zero levels.
Advantages of Magnetic Particle Inspection
Magnetic particle inspection has several advantages, which is why we use it so often on our ERW Steel Pipes:
- High Sensitivity: MPI can detect very small surface and near - surface defects. Even cracks that are just a few micrometers wide can be detected, which is crucial for ensuring the quality of our pipes.
- Fast and Cost - Effective: Compared to some other inspection methods, MPI is relatively quick and inexpensive. We can inspect a large number of pipes in a short time, which helps us keep our production costs down without compromising on quality.
- Visible Indications: The magnetic particle clusters form visible indications of the defects. This makes it easy for our inspectors to identify and evaluate the defects without the need for complex equipment or analysis.
Limitations of Magnetic Particle Inspection
Of course, no inspection method is perfect. Magnetic particle inspection has some limitations:
- Limited to Ferromagnetic Materials: MPI only works on ferromagnetic materials, like iron, nickel, and cobalt. If we're dealing with non - ferromagnetic materials, we have to use other inspection methods.
- Surface and Near - Surface Only: MPI can only detect surface and near - surface defects. Defects that are deeper inside the pipe may not be detected by this method. For deeper defects, we might use ultrasonic testing or radiographic testing.
- Requires Clean Surfaces: As I mentioned earlier, the pipe surface needs to be clean for accurate inspection. If the surface is dirty or has a lot of rust, the magnetic particles may not adhere properly, leading to false indications or missed defects.
Other Inspection Methods We Use
While magnetic particle inspection is a great method for detecting surface and near - surface defects, we also use other inspection methods to ensure the overall quality of our ERW Steel Pipes. For example, we use ultrasonic testing to detect internal defects, like laminations or voids. And for pipes that need to meet very high - quality standards, we might use radiographic testing, which can provide detailed images of the internal structure of the pipe. We also offer Premium ASTM B619/B626 Nickel Alloy Welded Pipe For Corrosion Resistance, which undergoes a comprehensive inspection process to ensure its corrosion - resistant properties.
Conclusion
In conclusion, magnetic particle inspection is an important part of our quality control process for ERW Steel Pipes. It helps us detect surface and near - surface defects quickly and accurately, ensuring that our pipes meet the highest quality standards. Whether you're in the construction industry, the oil and gas sector, or any other industry that requires high - quality pipes, you can trust our ERW Steel Pipes.


If you're interested in purchasing ERW Steel Pipes or have any questions about our inspection methods, feel free to reach out to us. We're always happy to have a chat and discuss your specific needs.
References
- ASNT (American Society for Nondestructive Testing). "Magnetic Particle Testing Handbook."
- ASTM International. "Standard Practices for Magnetic Particle Testing."