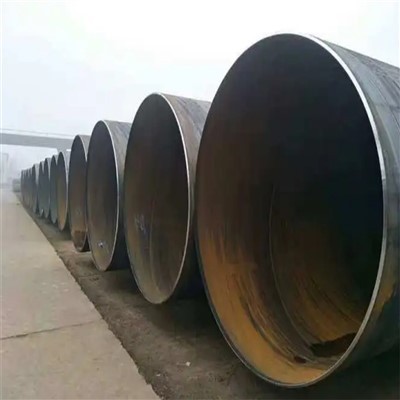
As a seasoned supplier of Seam Steel Pipe, I've witnessed firsthand the diverse welding methods that are crucial in the production of these essential industrial components. Seam steel pipes are widely used in various industries, including construction, oil and gas, and manufacturing, due to their strength, durability, and cost - effectiveness. In this blog, I'll delve into the different welding methods for seam steel pipes, highlighting their features, advantages, and applications.
1. Electric Resistance Welding (ERW)
Electric Resistance Welding is one of the most common methods for manufacturing seam steel pipes. In ERW, an electric current is passed through the edges of the steel strip or plate. The resistance to the current flow generates heat, which melts the edges. Then, the melted edges are pressed together to form a weld.


The main advantage of ERW is its high - speed production. It can produce pipes at a much faster rate compared to some other welding methods, which is ideal for large - scale manufacturing. ERW pipes are also known for their smooth inner and outer surfaces, which is beneficial in applications where fluid flow is a concern, such as in water supply systems.
Another advantage is the relatively low cost. Since it doesn't require additional filler materials, the production cost is reduced. ERW pipes are commonly used in structural applications, such as in building frames and scaffolding. For example, our A36 Black Mild Carbon Steel Tube is often produced using the ERW method. A36 steel is a popular choice for general structural use due to its good strength and weldability, and the ERW process can effectively join the steel to form high - quality pipes.
However, ERW has some limitations. The weld quality can be affected by factors such as the electrical conductivity of the steel and the uniformity of the current distribution. In some high - pressure or high - temperature applications, the weld strength of ERW pipes may not be sufficient, and other welding methods may be required.
2. Submerged Arc Welding (SAW)
Submerged Arc Welding is a welding process in which an arc is formed between a continuously fed electrode and the workpiece, and the arc is shielded by a layer of granular flux. The flux not only protects the weld from oxidation and contamination but also provides additional alloying elements to improve the weld quality.
One of the significant advantages of SAW is its high deposition rate. It can deposit a large amount of weld metal in a short time, making it suitable for thick - walled pipes. SAW can produce high - quality, strong welds with excellent mechanical properties. The welds are often free from porosity and have good fusion with the base metal.
SAW is widely used in the oil and gas industry for the production of large - diameter, high - pressure pipes. Our Api 5l Gr.B Steel Pipe is often manufactured using SAW. API 5L Gr.B steel is a standard for line pipes used in the transportation of oil and gas, and the high - quality welds produced by SAW ensure the integrity of the pipes in harsh environments.
However, SAW has some drawbacks. The process requires a relatively large amount of equipment and is more complex to operate compared to ERW. It also produces a large amount of slag, which needs to be removed after welding, adding to the production time and cost.
3. High - Frequency Induction Welding (HFIW)
High - Frequency Induction Welding is a specialized form of electric resistance welding. In HFIW, high - frequency electrical energy is used to heat the edges of the steel strip or plate. The high - frequency current is concentrated at the edges of the workpiece, generating intense heat for welding.
One of the main advantages of HFIW is its high - speed and precise welding. It can achieve very fast welding speeds, and the weld quality is highly consistent. HFIW can produce pipes with excellent weld strength and a narrow heat - affected zone, which reduces the distortion of the pipe.
HFIW is commonly used in the production of small - to medium - diameter pipes. Our Factory Supply Of A36 Straight Seam Pipe can also be manufactured using HFIW. The A36 steel, combined with the precise HFIW process, results in pipes that meet the high - quality standards required for various structural and industrial applications.
However, HFIW equipment is relatively expensive, and the process requires a high level of technical expertise to operate. Any small deviation in the process parameters can affect the weld quality.
4. Gas Tungsten Arc Welding (GTAW)
Gas Tungsten Arc Welding, also known as TIG (Tungsten Inert Gas) welding, uses a non - consumable tungsten electrode to produce the weld. An inert gas, such as argon, is used to shield the weld from oxidation.
The main advantage of GTAW is its high - quality welds. It can produce very clean and precise welds, with excellent control over the heat input and the amount of filler material (if used). GTAW is often used for welding thin - walled pipes or in applications where the appearance of the weld is important, such as in decorative or high - precision components.
However, GTAW is a relatively slow process, which makes it less suitable for large - scale production. The cost of the inert gas and the equipment is also relatively high.
5. Comparison and Selection of Welding Methods
When selecting a welding method for seam steel pipes, several factors need to be considered. The thickness of the pipe wall is a crucial factor. For thin - walled pipes, ERW or HFIW may be more suitable due to their high - speed and precise welding capabilities. For thick - walled pipes, SAW is often the preferred choice because of its high deposition rate and strong welds.
The application of the pipe also plays an important role. In applications where high pressure or high temperature is involved, such as in the oil and gas industry, SAW or other high - quality welding methods are required. In general structural applications, ERW pipes can meet the requirements in most cases.
Cost is another important consideration. ERW is the most cost - effective method for large - scale production, while GTAW is relatively expensive due to the slow process and the cost of the inert gas.
Conclusion
In conclusion, there are several welding methods available for seam steel pipes, each with its own advantages and limitations. As a Seam Steel Pipe supplier, we understand the importance of choosing the right welding method to meet the specific requirements of our customers. Whether it's the high - speed production of ERW, the strong welds of SAW, the precise welding of HFIW, or the high - quality finish of GTAW, we have the expertise and capabilities to produce high - quality seam steel pipes using the most appropriate method.
If you are in the market for Seam Steel Pipes and need more information about our products or the welding methods we use, please feel free to contact us for procurement and negotiation. We are committed to providing you with the best products and services to meet your industrial needs.
References
- AWS Welding Handbook, American Welding Society
- Steel Pipe Handbook, various industry experts
- Technical documents from steel and pipe manufacturing companies