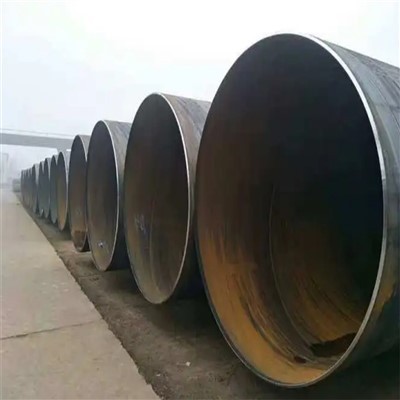
As a supplier of Submerged Arc Welded (SSAW) pipes, ensuring the quality and performance of our products is of utmost importance. One critical aspect of quality control is testing the pressure that these pipes can withstand. In this blog post, I will share some insights into how to test the pressure of SSAW pipes, which is essential for guaranteeing their safety and reliability in various applications.
Understanding the Importance of Pressure Testing
Pressure testing is a crucial step in the manufacturing and quality assurance process of SSAW pipes. These pipes are commonly used in a wide range of industries, including oil and gas, water supply, and construction. In these applications, the pipes are often subjected to high internal pressures. Therefore, it is necessary to verify that they can handle the specified pressure without leakage or failure.
Pressure testing helps to identify potential defects in the pipes, such as cracks, porosity, or weak welds. By subjecting the pipes to pressures higher than their normal operating conditions, we can ensure that they are structurally sound and meet the required standards. This not only protects the end - users from potential hazards but also enhances the reputation of our products in the market.
Types of Pressure Tests for SSAW Pipes
There are two main types of pressure tests commonly used for SSAW pipes: hydrostatic testing and pneumatic testing.
Hydrostatic Testing
Hydrostatic testing is the most widely used method for pressure testing SSAW pipes. In this test, the pipe is filled with water and then pressurized to a specified level. The test pressure is usually higher than the normal operating pressure of the pipe to ensure its integrity.
The process of hydrostatic testing involves the following steps:
- Preparation: First, the pipe is cleaned and inspected for any visible defects. Then, it is sealed at both ends with appropriate fittings.
- Filling with Water: The pipe is filled with water to remove any air inside. Air pockets can cause inaccurate pressure readings and may also lead to false test results.
- Pressurization: Once the pipe is filled with water, a pump is used to increase the pressure gradually to the test pressure. The pressure is maintained for a specified period, usually 5 - 10 minutes, to allow for any potential leaks to be detected.
- Inspection: During the test, the pipe is carefully inspected for any signs of leakage, such as water dripping or bubbling. If a leak is detected, the pipe is removed from the test and repaired or discarded.
- Depressurization: After the test is completed, the pressure is gradually released, and the water is drained from the pipe.
Hydrostatic testing has several advantages. Water is an incompressible fluid, which means that the pressure can be accurately controlled. It is also a relatively safe method, as water does not pose the same explosion risk as gases. Additionally, hydrostatic testing can detect both internal and external leaks.
Pneumatic Testing
Pneumatic testing involves pressurizing the pipe with air or another gas instead of water. This method is less commonly used than hydrostatic testing, but it may be preferred in some situations, such as when the pipe cannot be filled with water due to environmental or operational reasons.
The steps for pneumatic testing are similar to those of hydrostatic testing:


- Preparation: The pipe is cleaned, inspected, and sealed at both ends.
- Pressurization: A compressor is used to fill the pipe with air or gas and increase the pressure to the test level.
- Inspection: The pipe is inspected for leaks using a soap solution or other leak - detection methods. A soap solution will form bubbles at the location of a leak.
- Depressurization: After the test, the pressure is released, and the gas is vented from the pipe.
However, pneumatic testing has some disadvantages. Gases are compressible, which makes it more difficult to control the pressure accurately. It also poses a higher safety risk, as a sudden release of pressurized gas can cause an explosion. Therefore, strict safety precautions must be taken when conducting pneumatic tests.
Test Equipment and Standards
To conduct pressure tests on SSAW pipes, specialized equipment is required. For hydrostatic testing, a high - pressure water pump, pressure gauges, and valves are essential. For pneumatic testing, a compressor, pressure regulators, and leak - detection equipment are needed.
There are also various international and national standards that govern the pressure testing of SSAW pipes. For example, the American Petroleum Institute (API) has standards such as API 5L, which specifies the requirements for pressure testing of line pipes. The International Organization for Standardization (ISO) also has relevant standards, such as ISO 3183, which covers the technical delivery conditions for steel pipes for pipelines.
Compliance with these standards is crucial for ensuring the quality and safety of our SSAW pipes. We always make sure that our pressure testing procedures and equipment meet the requirements of these standards.
Factors Affecting Pressure Test Results
Several factors can affect the results of pressure tests on SSAW pipes.
Pipe Material and Thickness
The material and thickness of the pipe play a significant role in determining its pressure - bearing capacity. Different materials have different mechanical properties, such as yield strength and tensile strength. Thicker pipes generally have a higher pressure - bearing capacity than thinner pipes. During the design and manufacturing process, we carefully select the appropriate material and thickness based on the intended application of the pipe.
Weld Quality
The quality of the weld is another critical factor. SSAW pipes are welded using the submerged arc welding process, and any defects in the weld, such as lack of fusion or excessive porosity, can reduce the pipe's ability to withstand pressure. We have strict quality control measures in place during the welding process to ensure that the welds meet the required standards.
Temperature
Temperature can also affect the pressure test results. The mechanical properties of the pipe material can change with temperature. For example, at high temperatures, the yield strength of the steel may decrease, which can affect the pipe's pressure - bearing capacity. Therefore, it is important to conduct the pressure tests at a specified temperature range.
Applications of SSAW Pipes
SSAW pipes have a wide range of applications. They are commonly used in the oil and gas industry for transporting crude oil, natural gas, and refined products. In the water supply industry, SSAW pipes are used for water transmission and distribution networks. They are also used in construction projects for piling, structural support, and drainage systems.
If you want to learn more about the applications of similar pipes, you can visit LSAW Pipes And Their Applications. We also offer specific products like S275 SSAW 3PE Spiral Welded Steel Pipe and Spiral Welded Pipe With ASTM A252 Gr.1, which are suitable for different applications.
Conclusion
Pressure testing is an essential part of the quality control process for SSAW pipes. By using appropriate testing methods, equipment, and following the relevant standards, we can ensure that our pipes are safe and reliable for various applications. Whether it is hydrostatic testing or pneumatic testing, each method has its own advantages and disadvantages, and the choice depends on the specific requirements of the project.
As a SSAW pipe supplier, we are committed to providing high - quality products. Our pressure testing procedures are designed to meet the highest industry standards. If you are in need of SSAW pipes for your project, we invite you to contact us for procurement and further discussions. We are confident that our products will meet your expectations in terms of quality and performance.
References
- American Petroleum Institute (API). API 5L - Specification for Line Pipe.
- International Organization for Standardization (ISO). ISO 3183 - Petroleum and natural gas industries - Steel pipes for pipelines - Technical delivery conditions.