


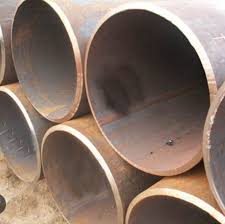
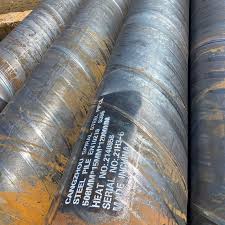
ASTM A252 Grade 1 Longitudinal Submerged Arc Welding (LSAW) Pipe
Basic Overview
ASTM A252 Grade 1 LSAW pipe is the entry-level grade in the ASTM A252 specification for welded and seamless steel pipe piles. It is a carbon steel pipe manufactured using the Longitudinal Submerged Arc Welding (LSAW) process, designed specifically for foundation piling and structural support applications where relatively lower strength requirements are acceptable .
Name Explanation
| Part | Meaning |
|---|---|
| ASTM | ASTM International (American Society for Testing and Materials) |
| A252 | Standard specification for welded and seamless steel pipe piles |
| Grade 1 | The lowest strength grade in the ASTM A252 specification – suitable for general structural purposes and light-load applications |
| Longitudinal Submerged Arc Welding (LSAW) | Manufacturing process – steel plates are formed and welded along a single straight longitudinal seam using submerged arc welding with filler metal added |
Key Features of ASTM A252 Grade 1 LSAW Pipe
| Feature | Description |
|---|---|
| Material Type | Low carbon steel – provides good weldability and adequate strength for foundation applications |
| Manufacturing | LSAW (Longitudinal Submerged Arc Welding) – plates formed by UOE, JCOE, or roll bending processes, then welded on inside and outside |
| Primary Application | Piling foundations, structural supports, light-load bearing members |
| Yield Strength | 205 MPa (30,000 psi) minimum |
| Tensile Strength | 345 MPa (50,000 psi) minimum |
| Elongation | 30% minimum (in 2 inches for wall thickness ≥5/16") |
| Typical Diameters (LSAW) | 304.8 mm to 1625.6 mm (12" to 64") |
| Typical Wall Thickness | 6 mm to 80 mm |
| Length | 6 m to 32 m standard; custom lengths available |
Chemical Composition (ASTM A252 Grade 1)
| Element | Heat Analysis (max %) | Product Analysis (max %) | Notes |
|---|---|---|---|
| Carbon (C) | 0.26 | 0.30 | Low carbon for weldability |
| Manganese (Mn) | 1.35 | 1.40 | Provides basic strength |
| Phosphorus (P) | 0.035 | 0.045 | Tight control for toughness |
| Sulfur (S) | 0.035 | 0.045 | Controlled for weld quality |
| Silicon (Si) | 0.45 max | Not specified | Deoxidizer |
Note: For each reduction of 0.01% below the specified maximum for carbon, an increase of 0.06% above the specified maximum for manganese is permitted, up to a maximum of 1.50% for heat analysis and 1.60% for product analysis .
Mechanical Properties Comparison: ASTM A252 Grades
| Property | Grade 1 | Grade 2 | Grade 3 |
|---|---|---|---|
| Yield Strength (min) | 205 MPa (30 ksi) | 240 MPa (35 ksi) | 310 MPa (45 ksi) |
| Tensile Strength (min) | 345 MPa (50 ksi) | 415 MPa (60 ksi) | 455 MPa (66 ksi) |
| Elongation (min) | 30% | 25% | 20% |
| Relative Strength | Baseline | +17% yield | +51% yield |
Sources:
LSAW Manufacturing Process for ASTM A252 Grade 1
Process Steps
| Step | Description |
|---|---|
| 1. Plate Selection | High-quality steel plates are selected according to ASTM A252 requirements |
| 2. Edge Preparation | Plate edges are beveled to create a V-shaped groove for welding |
| 3. Forming | Plates are formed into cylindrical shapes using UOE, JCOE, or press/roll bending machines |
| 4. Tack Welding | Formed plates are tack-welded to maintain shape before final welding |
| 5. Submerged Arc Welding | Multi-wire SAW applies internal weld, then external weld (double-sided) for full penetration |
| 6. Mechanical Expanding | Pipe expanded to precise dimensions to achieve tight tolerances and reduce residual stress |
| 7. Heat Treatment | May undergo stress relief heat treatment when specified |
| 8. Inspection & Testing | Non-destructive tests including ultrasonic examination and hydrostatic testing |
| 9. Finishing | End beveling (per ANSI B16.25), coating application as specified |
Forming Methods Available
| Method | Description | Suitability for Grade 1 |
|---|---|---|
| UOE | Plate pressed into U-shape, then O-shape, mechanically expanded after welding | Suitable |
| JCOE | Progressive J-C-O forming steps, expanded after welding | Suitable – high forming accuracy |
| Roll Bending | Plate progressively rolled into cylinder | Suitable for smaller production runs |
Size Availability
| Parameter | Range | Notes |
|---|---|---|
| Outside Diameter (LSAW) | 304.8 mm to 1625.6 mm (12" to 64") | Up to 84" (2134mm) from some manufacturers |
| Wall Thickness | 6 mm to 80 mm | Up to 100mm available from some manufacturers |
| Length | 6 m to 32 m | Custom lengths up to 70m available |
| End Finish | Plain ends, beveled ends per ANSI B16.25 | Beveled for welding standard |
Testing & Inspection Requirements
| Test Type | Purpose | Requirement |
|---|---|---|
| Chemical Analysis | Verify composition meets ASTM A252 limits | Per heat analysis |
| Tensile Test | Confirm yield and tensile strength | Per lot |
| Flattening Test | Check ductility | Required |
| Bend Test | Verify weld integrity | Required |
| Hydrostatic Test | Proof of leak-tightness | Each pipe tested |
| Ultrasonic Examination | Detect internal defects | 100% of weld seam when specified |
| Radiographic Examination (X-ray) | Verify weld quality | When specified |
| Dimensional Inspection | Verify OD, wall thickness, straightness | 100% |
| Visual Inspection | Surface condition, weld appearance | 100% |
Mill Test Certificate: EN 10204 / 3.1B typically provided
Applications of ASTM A252 Grade 1 LSAW Pipe
Grade 1 is specifically suited for lighter-duty structural applications where load requirements are relatively low:
| Application Area | Specific Uses |
|---|---|
| Building Foundations | Shallow foundation piles for small structures in hard clay strata with bearing capacity ≤120 kN/m² |
| Temporary Structures | Temporary shoring and excavation support |
| General Structural | Light-load bearing members, non-critical structural supports |
| Construction | General construction where higher grades (2 or 3) are not required |
Note: Grade 1 is the economical choice for projects where the calculated loads do not require the higher strength of Grade 2 or Grade 3 .
Coating & Protection Options
| Coating Type | Application |
|---|---|
| Black (bare) | Standard mill finish, indoor use |
| Varnish / Anti-rust oil | Temporary protection during transit |
| Black painting | Basic corrosion protection |
| FBE (Fusion Bonded Epoxy) | Corrosion protection for buried service |
| 3LPE (3-layer polyethylene) | Buried pipelines, harsh environments |
| Coal Tar Epoxy | Heavy-duty protection |
| Bitumen coating | Buried service |
| Galvanized | Outdoor exposed applications |
Comparison: ASTM A252 Manufacturing Types
| Aspect | LSAW (Longitudinal) | ERW | SSAW (Spiral) | Seamless |
|---|---|---|---|---|
| Weld Seam | Single straight seam | Single straight seam | Continuous spiral seam | No seam |
| Diameter Range | 12" to 64"+ | ≤ 24" typical | 8" to 120"+ | ≤ 24" typical |
| Wall Thickness | Up to 80 mm | Limited | Medium | Limited |
| Typical Application | Piling, foundations, structural | Smaller piling | Large diameter piling | Smaller piling, special applications |
Advantages of ASTM A252 Grade 1 LSAW Pipe
| Advantage | Description |
|---|---|
| Cost-Effective | Lowest cost option among ASTM A252 grades for projects with lower strength requirements |
| Large Diameter Capability | LSAW process enables production of large-diameter piles (up to 84") not possible with ERW or seamless |
| Thick Walls | Suitable for applications requiring substantial wall thickness (up to 80 mm) |
| High Structural Integrity | Single longitudinal seam with full-penetration double-sided welding ensures reliable performance |
| Excellent Dimensional Accuracy | Mechanical expanding achieves tight tolerances |
| Flexible Lengths | Can produce long piles (up to 32 m) reducing field splicing |
Important Selection Notes
1. Grade 1 vs. Higher Grades
Grade 1 is suitable for light-load applications, temporary structures, and projects with lower strength requirements
For most permanent foundation applications, Grade 2 is the most commonly specified grade
For heavy-duty, high-load projects, Grade 3 provides the highest strength
2. When to Choose ASTM A252 Grade 1 LSAW
Shallow foundations in competent soil
Temporary shoring and excavation support
Light structural applications
Projects where cost optimization is critical and loads permit lower strength
3. Manufacturing Process Selection
LSAW is preferred for:
Large diameters (≥12")
Thick wall applications
Projects requiring long pile lengths
When straight seam is specified
4. Corrosion Protection
For permanent structures, specify appropriate coating based on soil conditions
Options include FBE, 3LPE, coal tar epoxy, or bitumen coating
Galvanized available for above-ground applications
5. Certification
Standard: EN 10204 3.1 (manufacturer's independent testing)
Ensure Mill Test Certificate includes: chemical composition, mechanical properties, hydrostatic test results
6. Comparison with API 5L
ASTM A252 is specifically for piling/foundation applications, not for pressure service
API 5L is for oil/gas transmission pipelines
Yield strength of A252 Grade 1 (205 MPa) is lower than API 5L Grade B (241 MPa)
Temperature range for A252: -45°C to 100°C (Grade 3 mandates Charpy testing at -45°C)
Final Takeaway: ASTM A252 Grade 1 LSAW Pipe is the entry-level, large-diameter welded pipe pile for foundation applications with relatively low strength requirements. With minimum yield strength of 30,000 psi (205 MPa) , it offers an economical solution for light-load projects where higher-strength grades (Grade 2 or Grade 3) are not required. The LSAW manufacturing process enables production of pipes from 12" to 64" diameter with wall thicknesses up to 80 mm and lengths up to 32 m, making it a versatile option for various construction and foundation needs. Grade 1 is suitable for shallow foundations, temporary shoring, and general structural applications where cost optimization is important and calculated loads permit the use of the lowest strength grade . For permanent, high-load foundations, consider Grade 2 (most common) or Grade 3 (highest strength) instead .


