



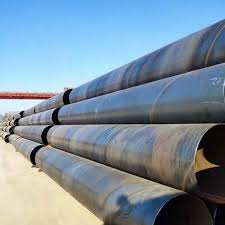
API 5L PSL2 Grade X52 is a standard, widely available, and commonly specified premium-grade product for manufacturing Spiral Submerged Arc Welded (SSAW) steel pipes [citation:1, citation:5, citation:10]. This combination is offered by numerous global manufacturers for critical oil and gas transmission, offshore pipelines, and high-pressure applications where enhanced quality and guaranteed toughness are required [citation:2, citation:5, citation:10].
The designation "API 5L PSL2 Grade X52 Spiral Submerged Arc Pipe" combines the widely-used X52 strength grade with the enhanced PSL2 quality level, produced using the economical spiral welding process for large-diameter, high-reliability applications [citation:2, citation:5, citation:10].
📋 Key Specifications for API 5L PSL2 Grade X52 SSAW Pipe
The table below summarizes the primary specifications for this product, based on comprehensive industry data [citation:1, citation:2, citation:5, citation:8, citation:10].
| Attribute | Description |
|---|---|
| Standard | API 5L: "Specification for Line Pipe" (aligned with ISO 3183) [citation:2, citation:5]. |
| Product Specification Level | PSL2: The enhanced quality level for line pipe, with stricter requirements than PSL1 including tighter chemistry controls, maximum strength limits, mandatory Charpy impact testing, and more stringent NDT [citation:2, citation:5, citation:10]. |
| Steel Grade | X52 (L360) : A medium-strength grade. The "X52" designation indicates a minimum yield strength of 52,000 psi (359 MPa) [citation:2, citation:4, citation:6]. |
| ISO Designation | L360 [citation:2, citation:8]. |
| Manufacturing Process | Spiral (Helical) Submerged Arc Welding (SSAW/HSAW) : Formed from hot-rolled steel coil, with the weld seam running continuously in a spiral along the pipe's length. Welded using double-sided automatic submerged arc welding with full penetration [citation:1, citation:5, citation:9, citation:10]. |
| Chemical Composition (max %) [citation:1, citation:2, citation:4, citation:8, citation:10] | Carbon (C): 0.22-0.24% max (tighter than PSL1's 0.26-0.28%) Manganese (Mn): 1.40% max Phosphorus (P): 0.025% max (tighter than PSL1's 0.030%) Sulfur (S): 0.015% max (50% reduction from PSL1's 0.030%) Niobium + V + Ti: 0.15% max Silicon (Si): 0.45% max |
| Mechanical Properties [citation:2, citation:3, citation:8, citation:10] | Yield Strength: 360-531 MPa (52,000-77,000 psi) range – both minimum and maximum specified Tensile Strength: 460-760 MPa (66,000-110,000 psi) range Yield-to-Tensile Ratio: ≤ 0.93 maximum Charpy Impact: Mandatory – typically 27-41J at specified temperature (often 0°C, -20°C, or -30°C) [citation:2, citation:3, citation:10] |
| Typical Size Range [citation:1, citation:5, citation:7, citation:9, citation:10] | Outside Diameter: 219 mm to 4064 mm (approx. 8" to 160") Wall Thickness: 3.2 mm to 40 mm (common range 5-26 mm) Length: 3 m to 18 m standard; up to 50 m available for specific applications |
| Key Testing Requirements [citation:2, citation:5, citation:10] | Mandatory Charpy Impact Testing at specified temperature Tensile Testing verifying both minimum and maximum limits Chemical Analysis with tighter PSL2 limits (especially S ≤0.015%) Flattening and Bend Tests for weld integrity 100% Non-Destructive Testing of weld seam (UT/RT) Hydrostatic Test each pipe Hardness Testing for sour service grades |
| Common Applications [citation:2, citation:5, citation:6, citation:9] | High-pressure oil and gas transmission pipelines; offshore pipelines; cold climate pipelines requiring guaranteed toughness; natural gas gathering and transmission; produced water lines; pipeline station piping; critical infrastructure; regulated pipelines (FERC, DOT, FEMSA lines). |
| Certification | Mill Test Certificate to EN 10204 Type 3.1 with full test results and traceability records. API monogram available from licensed mills [citation:1, citation:5]. |
📊 API 5L PSL2 Grade X52: Chemical and Mechanical Properties
Chemical Composition [citation:1, citation:2, citation:4, citation:8, citation:10]
| Element | PSL2 Specification | PSL1 Comparison |
|---|---|---|
| Carbon (C) | ≤ 0.22-0.24% | 0.26-0.28% (tighter control) |
| Manganese (Mn) | ≤ 1.40% | Same range |
| Phosphorus (P) | ≤ 0.025% | 0.030% (stricter) |
| Sulfur (S) | ≤ 0.015% | 50% reduction from PSL1's 0.030% |
| Nb+V+Ti | ≤ 0.15% | Not specified in PSL1 |
Mechanical Properties [citation:2, citation:3, citation:8, citation:10]
| Property | PSL2 Requirement | Significance |
|---|---|---|
| Yield Strength | 360-531 MPa | Both minimum AND maximum specified |
| Tensile Strength | 460-760 MPa | Both minimum AND maximum specified |
| Yield Ratio (Y/T) | ≤ 0.93 | Ensures adequate ductility |
| Impact Energy | ≥27-41J @ specified temp | Mandatory, unlike PSL1 |
📏 Dimensional Specifications
API 5L specifies the following tolerances for SSAW pipes [citation:1, citation:3, citation:7]:
| Parameter | Size Range | Tolerance |
|---|---|---|
| Outside Diameter | < 60.3 mm | -0.8 to +0.4 mm |
| 60.3 mm to 168.3 mm | ±0.0075D | |
| 168.3 mm to 610 mm | ±0.0075D (max ±3.2 mm) | |
| 610 mm to 1422 mm | ±0.005D (max ±4.0 mm) | |
| Wall Thickness | ≤ 5 mm | ±0.5 mm |
| 5 mm to 15 mm | ±0.1t | |
| ≥ 15 mm | ±1.5 mm | |
| Straightness | All sizes | ≤ 0.1% of total length |
Standard Diameter Range: 219mm to 4064mm (8" to 160") [citation:1, citation:5, citation:7, citation:10]
📊 Where X52 Fits Among API 5L PSL2 Grades
X52 is positioned as the most common "transition grade" between low-pressure gathering systems and high-pressure transmission pipelines [citation:2, citation:6]:
| Grade | Yield (min, MPa) | Yield (max, MPa) | Typical Application |
|---|---|---|---|
| B | 245 | 448 | Low-pressure gathering, utilities [citation:2, citation:3] |
| X42 | 290 | 496 | Gathering lines, distribution [citation:2, citation:3] |
| X46 | 317 | 524 | Medium-pressure gathering |
| X52 | 360 | 531 | Transmission, gathering, process - MOST COMMON [citation:2, citation:3] |
| X56 | 386 | 544 | Transmission pipelines |
| X60 | 414 | 565 | High-pressure transmission [citation:2, citation:3] |
| X65 | 448 | 600 | High-pressure, offshore [citation:2, citation:3] |
| X70 | 483 | 621 | Long-distance, high-pressure [citation:2, citation:3] |
| X80 | 552 | 690 | Ultra-high-pressure trunk lines [citation:2, citation:3] |
🔍 Key Points to Understand
What "PSL2 Grade X52" Means: This specification combines the widely-used X52 grade (360 MPa minimum yield) with the enhanced quality requirements of PSL2. The result is a pipe with 360 MPa minimum yield strength that also features guaranteed impact toughness, tighter chemistry controls (especially sulfur ≤0.015%), maximum strength limits (≤531 MPa), and full traceability [citation:2, citation:5, citation:10].
Why Choose PSL2 Grade X52? PSL2 Grade X52 is specified when [citation:2, citation:5, citation:10]:
Low-temperature service requires guaranteed impact properties (often -20°C to -45°C)
Project specifications mandate PSL2 quality (common for regulated pipelines)
Enhanced documentation and traceability are required by code
Maximum strength limits need control to prevent field welding issues
Sour service requires low sulfur content (≤0.015%)
Regulatory compliance (FERC, DOT, FEMSA lines) is required
Critical applications where the cost premium for PSL2 is justified
Impact Testing Temperature: Standard Charpy testing is at 0°C with 27J minimum, but lower temperatures (-20°C, -30°C, -45°C) can be specified for demanding applications [citation:2, citation:10]. Some manufacturers offer X52 with guaranteed impact at -30°C as standard .
Sour Service Option: For H₂S-containing environments, specify X52N or X52QS grades with supplementary requirements including hardness testing (≤248 HV10) and HIC/SSC testing per NACE MR0175/ISO 15156 [citation:2, citation:4].
SSAW Advantages for PSL2: The spiral welding process offers specific benefits for large-diameter PSL2 pipes [citation:5, citation:7, citation:10]:
Large Diameter Capability: Can economically produce pipes up to 160" diameter – SSAW is the only process that can efficiently produce diameters over 56" for X52 PSL2
Cost Efficiency: 20-30% lower cost than LSAW for very large diameters
Long Lengths: Up to 50m lengths reduce field welding requirements by up to 40%
Stress Distribution: Spiral weld seam disperses stress more evenly than straight seam
Weld Quality: Double-sided submerged arc welding ensures full penetration with 100% NDT
📝 PSL2 vs. PSL1 Comparison for X52 SSAW Pipe
The table below highlights the critical differences between PSL1 and PSL2 for X52, demonstrating why PSL2 is the premium choice [citation:2, citation:5, citation:8, citation:10]:
| Feature | PSL1 Grade X52 | PSL2 Grade X52 | Significance |
|---|---|---|---|
| Carbon (C) max | 0.26-0.28% | 0.22-0.24% | Better weldability, lower HAZ hardness |
| Sulfur (S) max | 0.030% | 0.015% | 50% reduction – critical for toughness and HIC resistance |
| Phosphorus (P) max | 0.030% | 0.025% | Improved toughness and weldability |
| Yield Strength | 360 MPa min only | 360-531 MPa range | Prevents over-strength materials that could cause welding issues |
| Tensile Strength | 460 MPa min only | 460-760 MPa range | Ensures consistent mechanical properties |
| Yield Ratio (Y/T) | Not specified | ≤ 0.93 | Ensures adequate ductility |
| Impact Testing | Not required | Mandatory (27-41J @ specified temp) | Guarantees low-temperature toughness |
| Carbon Equivalent | Not required | Calculated and controlled | Ensures good field weldability |
| Hardness Control | Not specified | ≤ 250 HV10 (sour: 248 HV10) | Essential for sour service applications |
| Best For | General service, water lines, temperate climates | Critical service, low-temperature, offshore, regulated pipelines |
🔧 Manufacturing Process for API 5L PSL2 Grade X52 SSAW Pipe
The manufacturing process follows enhanced PSL2 quality controls with additional testing and documentation requirements [citation:1, citation:9, citation:10]:
Raw Material Preparation: Hot-rolled steel coils meeting PSL2 chemistry requirements (especially low sulfur ≤0.015%) are leveled, inspected, and edge-milled. Each coil is identified for full traceability [citation:1, citation:10].
Spiral Forming: The steel strip is continuously formed into a cylindrical shape at a specific helix angle (typically 50-70°) at room temperature [citation:1, citation:5].
Submerged Arc Welding: Double-sided automatic submerged arc welding (inside and outside) creates the spiral seam with full penetration. Welding procedures are qualified per PSL2 requirements with strict parameter control [citation:1, citation:9].
Non-Destructive Testing: 100% ultrasonic (UT) and/or radiographic (RT) inspection of the entire weld length with PSL2 acceptance criteria. Modern facilities use automated continuous UT systems [citation:1, citation:5, citation:10].
Hydrostatic Testing: Each pipe individually tested to verify pressure integrity; test parameters are automatically controlled and recorded with pressure-time charts [citation:1, citation:5].
Mechanical Testing: Tensile tests (verifying both min and max limits), flattening tests, bend tests, and mandatory Charpy impact testing on base metal, weld, and HAZ at specified temperature [citation:2, citation:5, citation:10].
End Finishing: Ends prepared (plain or beveled per ASME B16.25) for field welding; end face perpendicularity controlled to ≤3mm [citation:1, citation:9].
Coating: Optional external coatings (3LPE, FBE, 3LPP, coal tar epoxy) and internal linings available for corrosion protection [citation:1, citation:9, citation:10].
🏭 Applications and Selection Rationale
API 5L PSL2 Grade X52 SSAW pipes are used in demanding applications where enhanced quality is required [citation:2, citation:5, citation:6, citation:9, citation:10]:
| Application | Why PSL2 Grade X52 is Specified | Typical Requirements |
|---|---|---|
| High-Pressure Gas Transmission | Guaranteed Charpy impact toughness at 0°C to -30°C ensures ductile behavior in winter conditions; maximum strength limits prevent welding issues | Impact testing at -20°C, 100% NDT |
| Offshore Pipelines | Tight sulfur control (≤0.015%) provides HIC resistance; full traceability required; yield strength range ensures consistent properties | S ≤0.015%, PSL2 certification, third-party inspection |
| Cold Climate / Arctic Pipelines | Impact testing at -45°C ensures fracture resistance in extreme low temperatures; superior toughness of PSL2 grades | Charpy at -45°C, DWTT testing |
| Regulated Pipelines | FERC/DOT jurisdictions often require PSL2 quality for all pipeline materials; maximum yield strength prevents over-matching in welds | Full documentation, PSL2 certification |
| Sour Service | Low sulfur content (≤0.002% for sour grades) with hardness testing (≤248 HV10) meets NACE MR0175 requirements | HIC/SSC testing, hardness survey |
| Pipeline Station Piping | Complex fabricated components require consistent material properties and guaranteed toughness | PSL2 certification, impact testing |
| Subsea Pipelines | Critical applications demand PSL2's enhanced testing, traceability, and quality control | PSL2, DWTT, CTOD testing |
📝 Important Considerations
Cost Premium: PSL2 Grade X52 typically costs 10-20% more than PSL1 Grade X52 due to additional testing, tighter chemistry controls, and enhanced documentation requirements. The premium is justified for applications where guaranteed performance is essential .
Availability: PSL2 Grade X52 is readily available from major manufacturers worldwide, as it is one of the most commonly produced PSL2 grades [citation:1, citation:5, citation:9, citation:10].
Heat Treatment Designation: X52 PSL2 may include suffixes indicating heat treatment [citation:2, citation:4]:
X52N: Normalized (for improved grain structure and uniform properties)
X52M: Thermomechanically rolled (TMCP – for enhanced toughness and weldability)
X52Q: Quenched and tempered (for maximum strength uniformity)
International Equivalents: X52 PSL2 has several international equivalents :
EN 10208-2 L360NB/MB
DIN 17172 StE 360.7 TM
GB/T 9711 L360 PSL2
ISO 3183 L360
Complete Specification: When ordering, specify [citation:5, citation:9, citation:10]:
API 5L PSL2, Grade X52, SSAW (spiral welded), Size (OD x WT), Length, End Finish
Impact Test Temperature: [e.g., 0°C, -20°C, -30°C, -45°C]
Heat treatment: [N, M, Q] if required
Any supplementary requirements (sour service, additional NDT, hardness testing)
Coating requirements: [e.g., 3LPE, FBE, 3LPP]
🛡️ Coating Options for Corrosion Protection
API 5L PSL2 X52 spiral pipes can be supplied with various coatings depending on the application environment [citation:1, citation:9, citation:10]:
| Coating Type | Best For | Key Features | Typical Thickness |
|---|---|---|---|
| 3LPE (3-layer polyethylene) | Underground pipelines | Excellent corrosion protection, high impact resistance, good adhesion | 2.5-3.7 mm |
| FBE (Fusion Bonded Epoxy) | Oil & gas pipelines | Strong adhesion, chemical resistance, smooth surface | 300-600 μm |
| 3LPP (3-layer polypropylene) | Offshore pipelines | High temperature resistance (up to 140°C), excellent mechanical strength | 2.5-3.7 mm |
| Coal Tar Epoxy | Marine environments | Cost-effective, high moisture resistance | 400-600 μm |
| Internal Epoxy Coatings | Corrosive media | Reduces friction, prevents corrosion, improves flow efficiency | 250-500 μm |
💰 Pricing Considerations (2025 Estimates)
Based on market data, API 5L PSL2 X52 spiral pipes typically range from $750 to $1,350 per ton depending on wall thickness and specifications :
| Wall Thickness | Price Range (USD/ton) | Typical Applications |
|---|---|---|
| 6-10 mm | $750 – $1,050 | Gathering lines, water transmission |
| 12-18 mm | $1,000 – $1,350 | High-pressure transmission, offshore |
| 20-26 mm | $1,300 – $1,700 | Deepwater, arctic, critical service |
Note: Prices vary based on order quantity, coatings, impact test temperature, and destination.
📝 Summary
API 5L PSL2 Grade X52 Spiral Submerged Arc Welded pipes are the standard, premium-quality choice for demanding pipeline applications worldwide [citation:2, citation:5, citation:10]. With minimum yield strength of 360 MPa (52,000 psi), these pipes combine the reliable mechanical properties of X52 – the most common transmission grade – with the premium features of PSL2: guaranteed Charpy impact toughness, tighter chemistry controls (especially sulfur ≤0.015%), maximum strength limits (≤531 MPa), full traceability, and more stringent testing [citation:2, citation:5, citation:8, citation:10].
Available in diameters from 219mm to over 4000mm with wall thicknesses to 40mm and lengths up to 50m, these pipes are produced using the cost-effective SSAW manufacturing process while meeting the rigorous requirements of the API 5L specification [citation:1, citation:5, citation:7, citation:10].
PSL2 Grade X52 is the preferred specification for [citation:2, citation:5, citation:6, citation:9, citation:10]:
High-pressure gas transmission requiring guaranteed impact properties
Offshore and marine applications with strict chemical controls
Cold climate and arctic pipelines requiring impact testing at -30°C to -45°C
Regulated pipelines (FERC, DOT, FEMSA) where PSL2 is mandatory
Sour service applications when specified with supplementary requirements
Critical infrastructure projects where enhanced documentation is required
When ordering, ensure you clearly indicate API 5L PSL2 Grade X52, SSAW, along with required dimensions, impact test temperature, and any coating or supplementary requirements based on your specific application [citation:5, citation:9, citation:10].


