


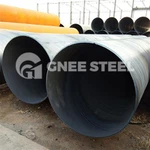


EN 10217-2 P265GH Welded Steel Tubes
Wall Thickness: 1.7mm-36mm
OD:10.3mm-609.6mm
Length: 5000mm-12000mm
in one-stop service
GNEE Group is a well-known Chinese manufacturer and supplier of EN10217 P265GH welded pipes. Our P265GH steel pipes are suitable for high-temperature and high-pressure environments, including boilers and pressure vessels. We prioritize quality and adhere to the production and testing of P265GH steel pipes according to various international standards. We produce P265GH high-frequency welded pipes with O.D.: 219mm-4064mm and WT: 3.2mm-30mm. If you require P265GH steel pipes or wish to learn more, please feel free to contact us.

EN10217 P265GH Pipe Specification
| Specification | EN10217-2 |
| Material | P265GH(1.0425), P195GH(1.0348), P235GH(1.0345), 16Mo3(1.5415) |
| Outer Diameter | 219mm-4064mm |
| Wall Thickness | 3.2mm-30mm |
| Surface treatment | Painting, oil coating, Anti-corrosion & Insulation |
| Ends | Pipe cap, Beveled edges or plain end, the protection of pipe end, anyway according to customers' requirement |
| Package | Bulk cargo, pipe cap, steel strips bundled |
| Delivery time | According to the quantity |
| Payment Term | T/T, L/C |
| Mechanical properties | ||
|---|---|---|
| Yield strength Rp0,5 MPa (in PSI): | Min: 265 (38 400)** | Max: - |
| Tensile strength Rm MPa (in PSI): | Min: 410 (59 500) | Max: 570 (82 700) |
| Elongation (% min.): | transverse: 21 | longitudinal: 23 |
| Impact strength | ||
| Test temperature in °C | 0 | |
| Min. average impact energy in J | transverse: 27 | longitudinal: 40 / 28 |
| Hardness (max. HRC) | - |
EN10217-2 P265GH HFW Pipe


GNEE P265GH Pipe for Sale
- P265GH Welded Spiral Steel Pipe
- P265GH SAWL Pipe
- P265GH High Frequency Welded Pipe
- P265GH Welded Steel Tube
- P265GH ERW Steel Pipe
GNEE P265GH LSAW Pipe Production Process
Longitudinal welded steel pipes are produced by feeding a certain specification of strip steel coil into a round pipe shape through a high-frequency welding machine unit, where the longitudinal seam is welded to form the steel pipe. The shape of the pipe can be round, square, or irregular, depending on the diameter rolling after welding. The specific process involves opening and straightening the end of the steel coil and feeding it into subsequent equipment. After uncoiling, the strip steel is leveled, the ends are trimmed, and the strip is sheared with a circular disc cutter before recoiling. The raw material from the steel mill is of a specific width, which is cut to the corresponding width based on the actual length of the pipe. During welding, I-shaped bevels are typically used to ensure uniform heating along the thickness direction and facilitate bevel preparation. After uncoiling, the strip steel is further leveled, the ends are trimmed, and scarfing (butt welding) is performed to ensure the continuous production of the forming unit. The prepared strip steel enters the continuous forming unit, where it is gradually bent into a round pipe by the action of squeeze rollers. The edges of the strip steel are heated by a high-frequency welding machine to welding temperature, then pressure welded by squeeze rollers. Subsequently, scarfing removal devices are used to remove internal and external burrs formed by the melting or plastic state of the metal squeezed onto the inner and outer surfaces of the pipe. After a period of air cooling, the pipe is water-cooled to prevent bending deformation due to air cooling. The steel pipe produced by the squeeze rollers has a certain ellipticity in its cross-section, with the outer diameter slightly larger than the finished pipe. To obtain precise outer diameter and cross-sectional shape of the steel pipe, cold sizing is performed on the welded pipe by a sizing machine after water cooling. The sized welded pipe is then cut into specified or multiple length sections while in motion, meeting the corresponding tolerance requirements.
P265GH Welded Pipe Test

- Visual inspection
- Chemical element testing
- Physical property testing
- Non-destructive testing (NDT)
- Ultrasonic testing
- eddy current testing
- etc.
Hot Tags: en 10217-2 p265gh welded steel tubes, China en 10217-2 p265gh welded steel tubes manufacturers, suppliers, API 5L PSL2, straight seam submerged arc welded SAWL steel pipe, GB T1591 2009, JIS G3101, SAWL Carbon Steel Tube, A335 Alloy Steel ERW Pipe
You Might Also Like


Send Inquiry