


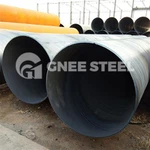


SY/T5037 Spiral Steel Pipe
Type: Spiral Steel Pipe
OD: 219mm -4064mm
WT: 3.2-40mm
Length: 3m-48m
SY/T5037 SSAW Pipe Description
SY/T5037 standard specifies the dimensions, shape, quality, performance requirements, test methods, inspection rules, coatings, markings, and quality certificates for submerged arc welded steel pipes for ordinary fluid transportation (including straight seam and spiral seam submerged arc welded steel pipes, hereinafter referred to as "steel pipes"). SY/T5037 spiral welded pipes are suitable for transporting common fluids such as water, air, and heating steam.
The nominal outside diameter range for SY/T5037 steel pipes is no less than 219.1mm, and the nominal wall thickness range is t≥3.2mm. The nominal outside diameter and wall thickness of the steel pipes should comply with the relevant requirements of SY/T6475. If you require other specifications of SY/T5037 steel pipes, GNEE Group can also supply welded pipes of other diameters and wall thicknesses.
SY/T5037 Spiral Submerged Arc Welding Pipe Specification
| OD | 219mm -4064mm |
| WT | 3.2-40mm |
| Length | 3m-48m |
| Origin | China |
| Test | Chemical Component Analysis, Mechanical Properties (Ultimate Tensile Strength, Yield Strength, Elongation), Technical Properties (Flattening Test, Bending Test, Impact Test), Exterior Size Inspection, Hydrostatic Test, X-ray Test. |
SY/T5037 SSAW Steel Pipe


Inspection of SY/T5037 Steel Pipes
- Chemical Composition
1. Samples for chemical analysis can be taken from finished steel pipes or steel strips/plates. When sampling from steel strips/plates, the sampling method should comply with the sampling provisions of the steel strip/plate standard. When sampling from steel pipes, the sampling location should be no less than 1/4 of the distance between adjacent spiral welds, or approximately 90° from the straight weld.
2. Chemical composition analysis should be conducted in accordance with the relevant parts of GB/T4336 or GB/223. In case of disputes, the results of wet chemical analysis shall prevail.
- Tensile Test
1. Tensile test samples for welded joints should be taken perpendicular to the weld. The weld should be in the middle of the sample, and should meet the requirements of Figure 3, with the weld reinforcement removed. It is allowed to flatten the sample at room temperature.
2. Except as specified in this standard, the tensile test should be conducted in accordance with GB/T2651, with a test temperature of 23℃±5℃ (or room temperature).
- Impact Test
The impact test should be conducted in accordance with GB/T229.
- Guided Bend Test
The guided bend test should be conducted in accordance with GB/T2653.
- Hydrostatic Test
The hydrostatic test should be conducted in accordance with GB/T241.
- Acid Etching Inspection of Welded Joints
1. Acid etching inspection of fracture surfaces of spiral and straight welded joints should be carried out as soon as possible after the weld is completed.
2. Acid etching samples should be taken from the pipe end using a gas cutting method. The acid etching surface should be ground so that the fusion line can be clearly observed after etching. The sample should not be hammered or deformed before the test.
- Non-destructive Testing
1. X-ray Inspection
The inspection method should comply with Appendix A or other standards equivalent to Appendix A.
2. Ultrasonic Testing
2.1. Ultrasonic testing of welds should comply with SY/T6423.2.
2.2. Ultrasonic testing of the 25mm wide area at the pipe ends should comply with SY/T6423.4.

Hot Tags: sy/t5037 spiral steel pipe, China sy/t5037 spiral steel pipe manufacturers, suppliers, GB T 14291 Welded Steel Pipe, Spiral Submerged Arc Welded Pipe, SY T5037 standard spiral steel pipe, A139 SSAW PIPE, SSAW Steel Pipe, JIS A5525 SSAW Pipe
You Might Also Like


Send Inquiry