




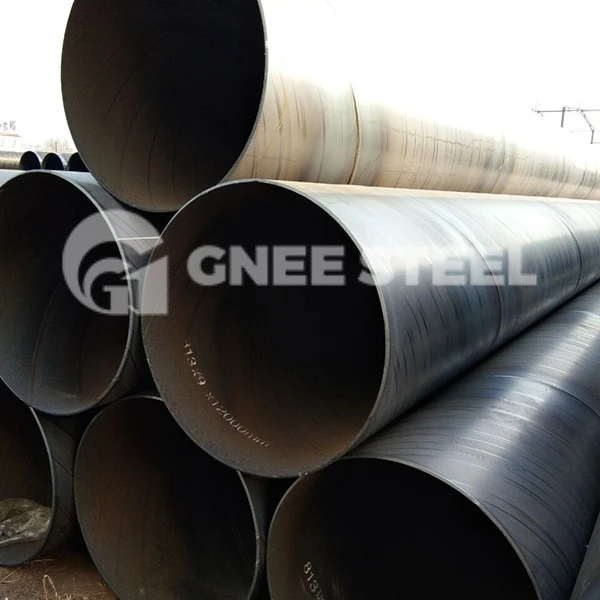
EN10219 Spiral Welding Pipe Description
EN10219 standard applies to non-alloy and fine-grain non-alloy cold-formed welded and seamless steel pipes. This standard specifies the size and shape requirements for spiral steel pipes. The size range for EN10219 spiral steel pipes includes an outer diameter from 219mm to 3048mm and a wall thickness from 5mm to 25mm.
EN10219 Spiral Welded Steel Pipe Specification
| Standard | EN10219 |
| Grade | S235JR,S275JR,S275J0H,S275J2H,S355JR,S355J0H,S355J2H,S460NH,S460NH |
| OD | 219 – 1820mm |
| WT | 5.0 -50mm |
| L | UP to 12m |
| Ends | Plain end/Beveled, protected by plastic caps on both ends, grooved, threaded and coupling, etc. |
EN10219 SSAW Steel Pipe Chemical Composition
|
Steel Grade |
% by mass, Maximum |
|||||
|
C |
Si |
Mn |
P |
S |
N |
|
|
S235JRH |
0.17 |
- |
1.40 |
0.040 |
0.040 |
0.009 |
|
S275JOH |
0.20 |
- |
1.50 |
0.035 |
0.035 |
0.009 |
|
S275J2H |
0.20 |
- |
1.50 |
0.030 |
0.030 |
- |
|
S355JOH |
0.22 |
0.55 |
1.60 |
0.035 |
0.035 |
0.009 |
|
S355J2H |
0.22 |
0.55 |
1.60 |
0.030 |
0.030 |
- |
|
S355K2H |
0.22 |
0.55 |
1.60 |
0.030 |
0.030 |
- |
EN10219 Welded Pipe


Delivery Conditions for EN10219 Welded Pipes
Cold-formed hollow sections cannot undergo heat treatment, except during the welding process where the temperature may become excessively high. Note: For SAW hollow sections with an outer diameter above 508mm, heat-forming operations must be performed, but the mechanical properties will not be affected.
Quality assurance requirements are detailed in EN 10021. If customers have special quality assurance requirements, they should refer to the EN ISO 9002 standard.
Tensile Testing
Tensile testing should adhere to the following provisions:
- For circular pipes, rectangular pipes, and square pipes, the test section can be an integral part of the product.
- Circular pipes do not require testing of the entire section; specimens are selected longitudinally or from the opposite end of the weld.
- Square pipes and rectangular pipes do not require testing of the entire section; specimens are selected longitudinally, at the corners, or from the opposite side of the weld.
- Additionally, cross-sectional testing can be conducted upon manufacturer request.
Impact Testing
Impact testing follows the following guidelines:
For circular pipes, testing is conducted longitudinally from the far end of the weld and longitudinally. Additionally, cross-sectional testing can be conducted upon manufacturer request.
For square pipes and rectangular pipes, specimens are selected longitudinally, at the corners, or from the opposite side of the weld. Additionally, cross-sectional testing can be conducted upon manufacturer request.
Hot Tags: en10219 ssaw steel pipe, China en10219 ssaw steel pipe manufacturers, suppliers, API 5L X52 PSL2 Spiral Welded Pipe, GB T 14291 SSAW Pipe, Carbon Spiral Welded Steel Pipe Tube, large diameter steel pipes, Spiral Welded Steel Pipe, SSAW Carbon Steel Tube
You Might Also Like


Send Inquiry