




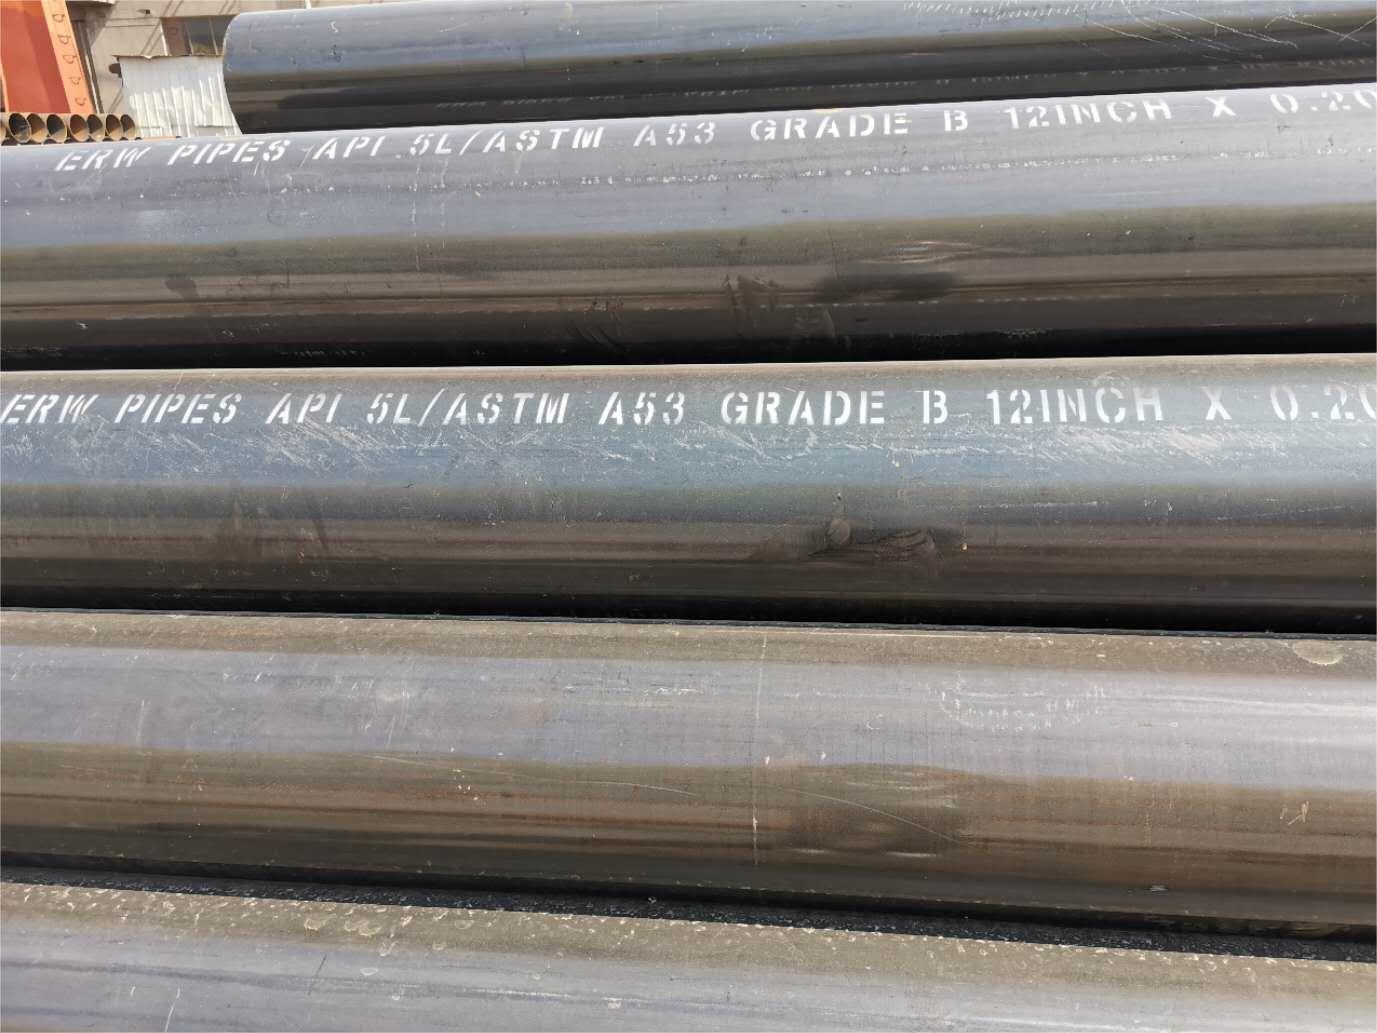
A53 Electric- Resistance Welded Pipe
A53 Pipe Specifications
Gnee Steel Products stock a full range of A/SA53-B welded pipe in:
Sizes: 1/8" NPS to 26" OD
Schedules: S/10, S/20, S/40, STD, S/60, S/80, XH, S/100, S/120, S/140, S/160 and XXH
Scope
ASTM A53 and ASME SA53 is intended for mechanical and pressure applications and is also acceptable for ordinary uses in steam, water, gas and air lines. It is suitable for welding and for forming operations involving coiling, bending, and flanging, subject to certain qualifications.
Looking for specific post-production services? See our full list.
Materials and Manufacture
The welded pipe shall be made by the following processes: open-hearth, electric furnace, or basic-oxygen. The weld seam of electric-resistance welded pipe in Grade B shall be heat treated after welding.
Chemical Requirements
| Type E | Type F | ||||
| (electric- resistance welded) |
(furnace- welded pipe) |
||||
| Grade A | Grade B | Grade A | |||
| Carbon max. % | 0.25 | 0.30* | 0.3 | ||
| Manganese % | 0.95 | 1.2 | 1.2 | ||
| Phosphorous, max. % | 0.05 | 0.05 | 0.05 | ||
| Sulfur, max. % | 0.045 | 0.045 | 0.045 | ||
| Copper, max.% | 0.40 | 0.40 | 0.4 | ||
| Nickel, max. % | 0.40 | 0.40 | 0.4 | ||
| Chromium, max. % | 0.40 | 0.40 | 0.4 | ||
| Molybdenum, max. % | 0.15 | 0.15 | 0.15 | ||
| Vanadium, max. % | 0.08 | 0.08 | 0.08 | ||
| *For each reduction below 0.01% below the specified carbon maximum, an increase of 0.06% manganese above the specified maximum will be permitted up to a maximum of 1.65% (does not apply to SA53). | |||||
Permissible Variations in Wall Thickness
The minimum wall thickness at any point shall not be more than 12.5% under the nominal wall thickness specified.
Permissible Variations in Weights per Foot
Plus or minus 10%
Permissible Variations in Outside Diameter
Outside Diameter at any point shall not vary from standard specified more than:
Tensile Requirements
| Electric-resistance-welded | Continuous-Welded | |||
| Grade A | Grade B | |||
| Tensile Strength, min., psi | 48,000 | 60,000 | 45,000 | |
| Yield Strength, min., psi | 30,000 | 35,000 | 25,000 | |
Hydrostatic Testing
Hydrostatic inspection test pressures for plain end and threaded and coupled pipe are specified. Hydrostatic pressure shall be maintained for not less than 5 seconds for all sizes of seamless and electric-resistance-weld pipe.
Mechanical Tests Specified
Tensile Test - Transverse required on ERW for NPS 8 and larger.
| Degree of Bend | Diameter of Mandrel | ||
| For Normal A53 Uses | 90 | 12 x nom dia. of pipe | |
| For Close Coiling | 180 | 8 x nom dia. of pipe |
Flattening Test - NPS 2 and larger XM and lighter walls.
Lengths
| Standard Weight | |
| Single Random - 16′ – 22′. 5% may be jointers. If Plain Ends - 5% may be 12′ – 16′. | |
| Double Random - Shortest Length 22′, minimum average for order 35′. | |
| Extra Strong and Double Extra Strong | |
| Single Random - 12′ -22′. 5% may be 6′ – 12′. | |
| Double Random (XS and lighter) - Shortest Length 22′, minimum average for order 35′. | |
| Lengths longer than single random with wall thicknesses heavier than XS subject to negotiation. | |
Required Markings on Each Length
(On Tags attached to each Bundle in case of Bundled Pipe)
Hot Tags: a53 electric- resistance welded pipe, China a53 electric- resistance welded pipe manufacturers, suppliers, Pipe Roll 8 Inch, Electrofusion Welded Carbon Steel Pipe, Seamless Pipe, Electrofusion Welding Plastic Pipe, Black Plastic Underground PE Water, EFW Pipe
Previous
EN 10210-1 Grade S420NH PipeYou Might Also Like




Send Inquiry